Pharaon Plastic

Our Factory

Manufacturing

One plant in production, a second in development

Everything below is a machine count or a measured area, so you can size an order against it.

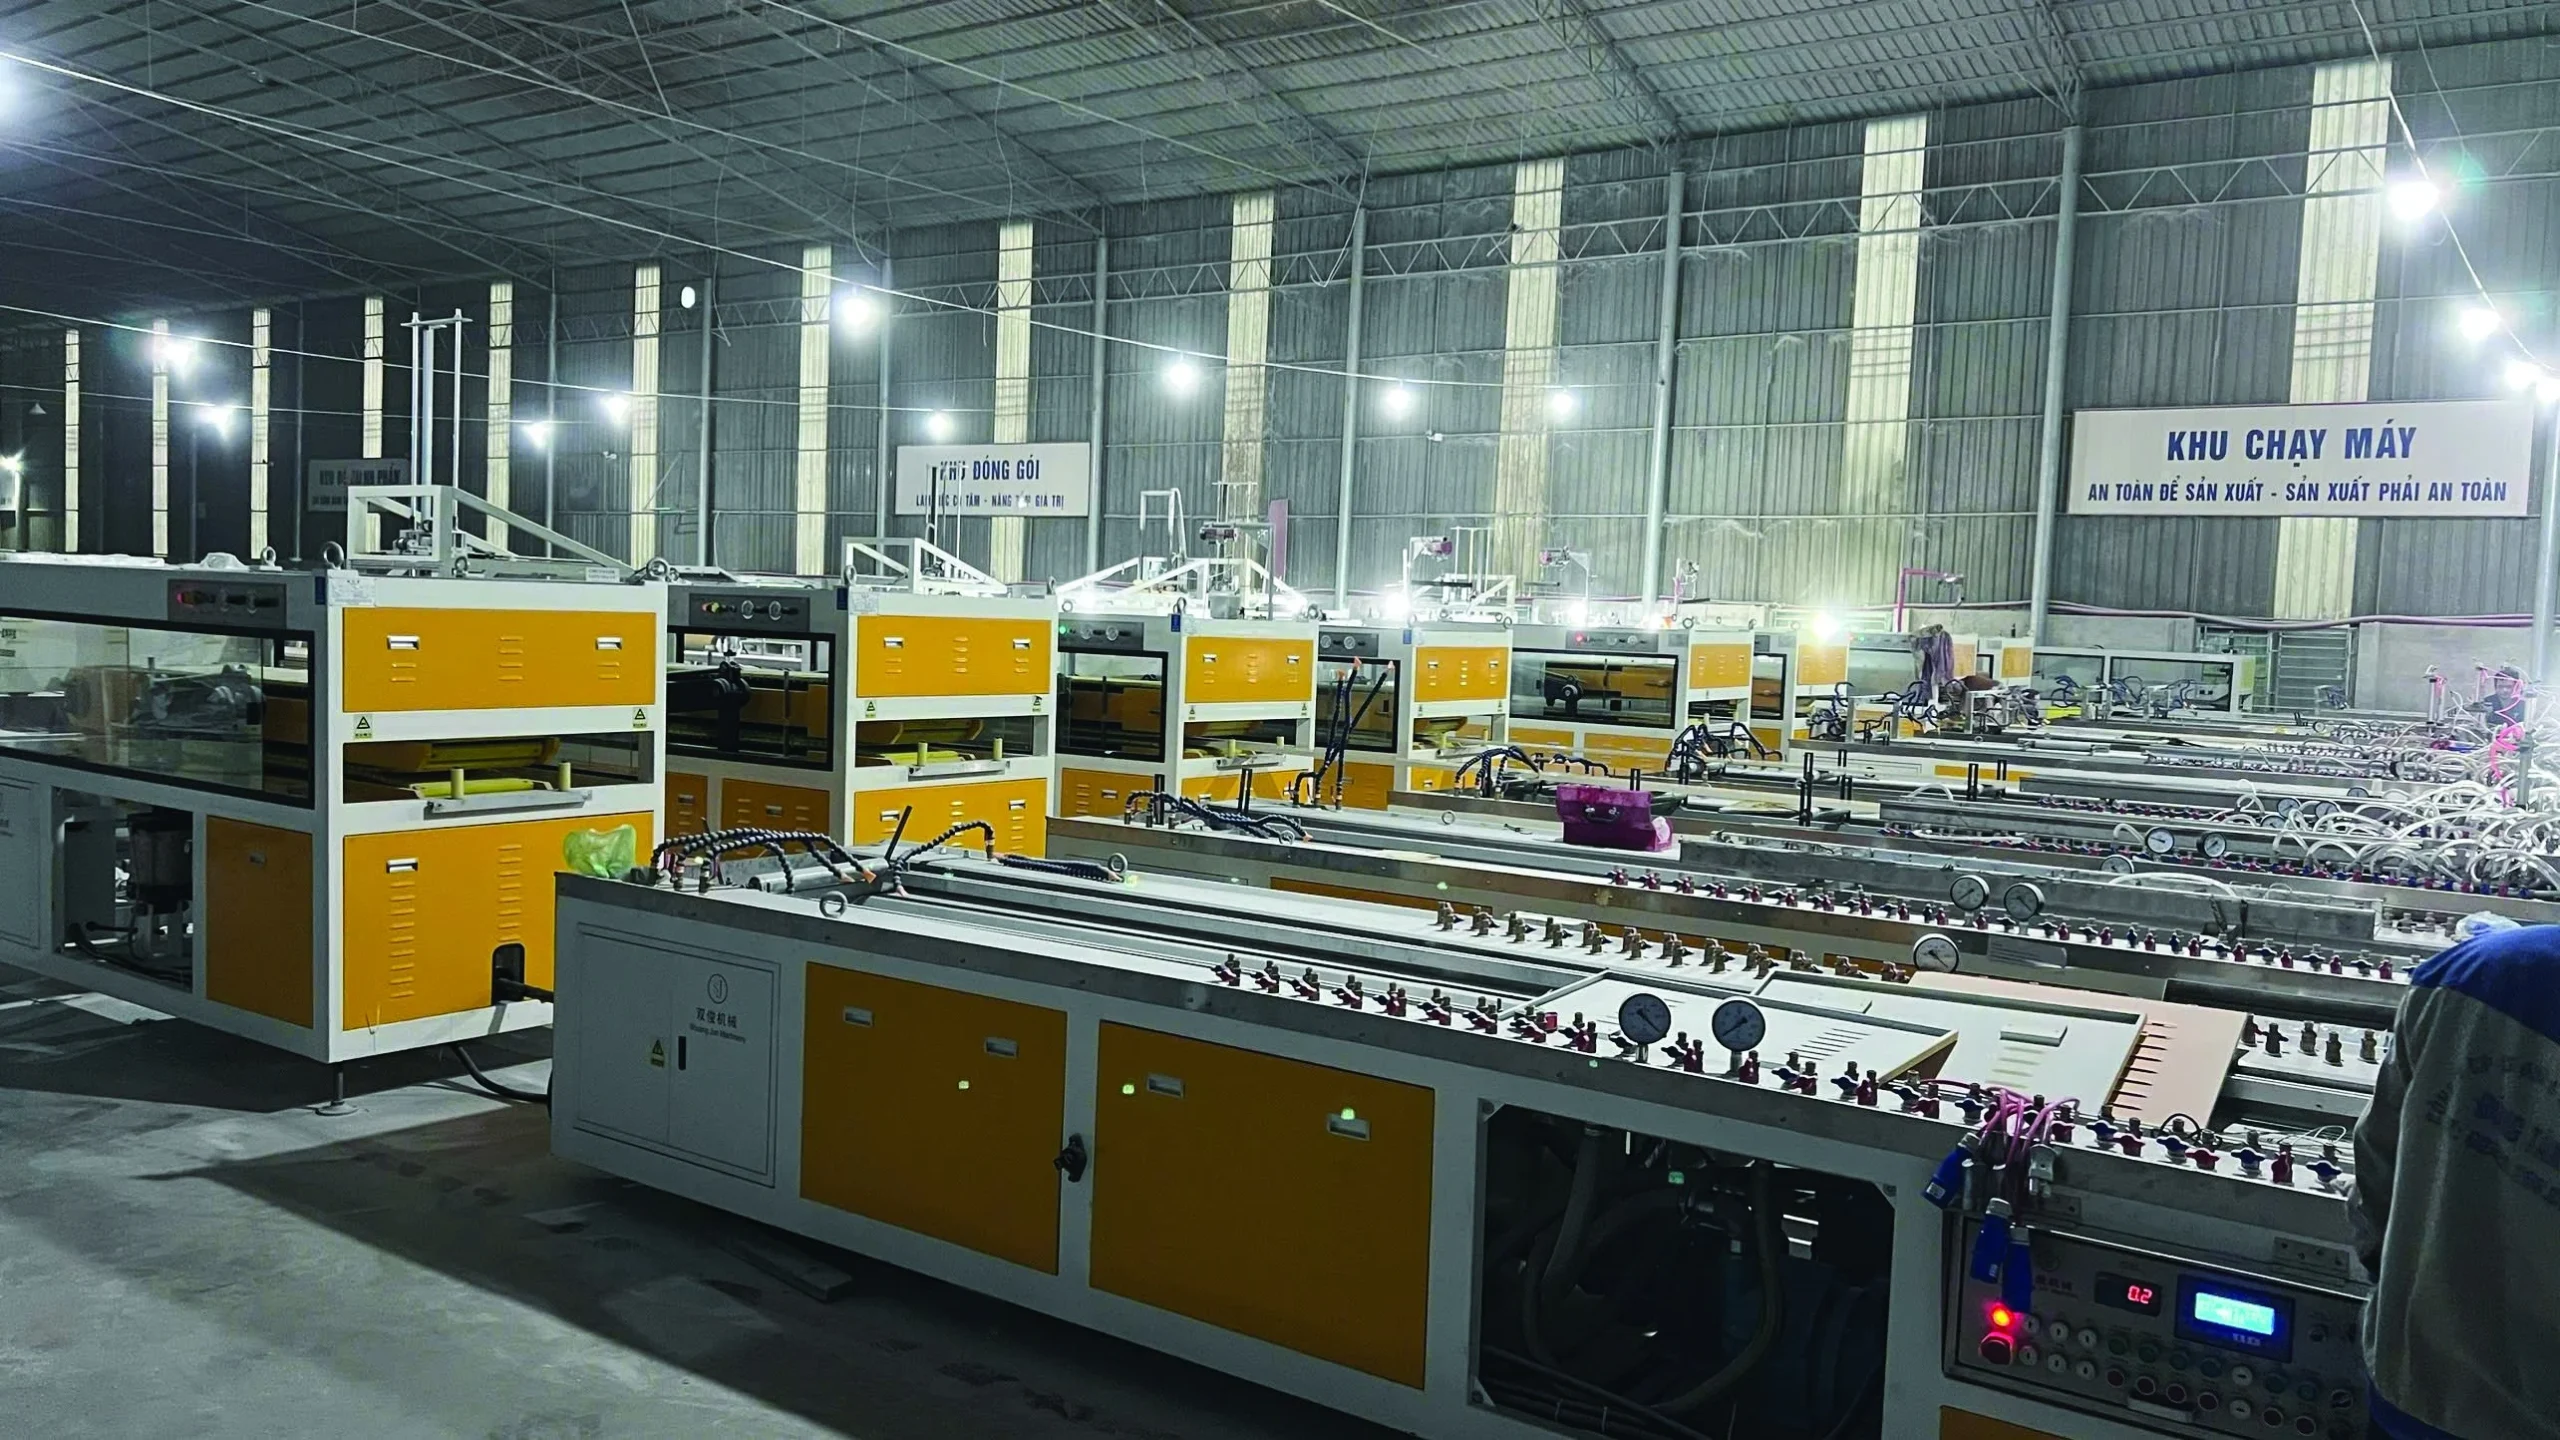
Pharaon PVC and WPC wall panel factory production line in Vietnam
Extrusion

25 nano lines

High-speed nano extrusion systems, plus one stone-grain PVC extrusion line.
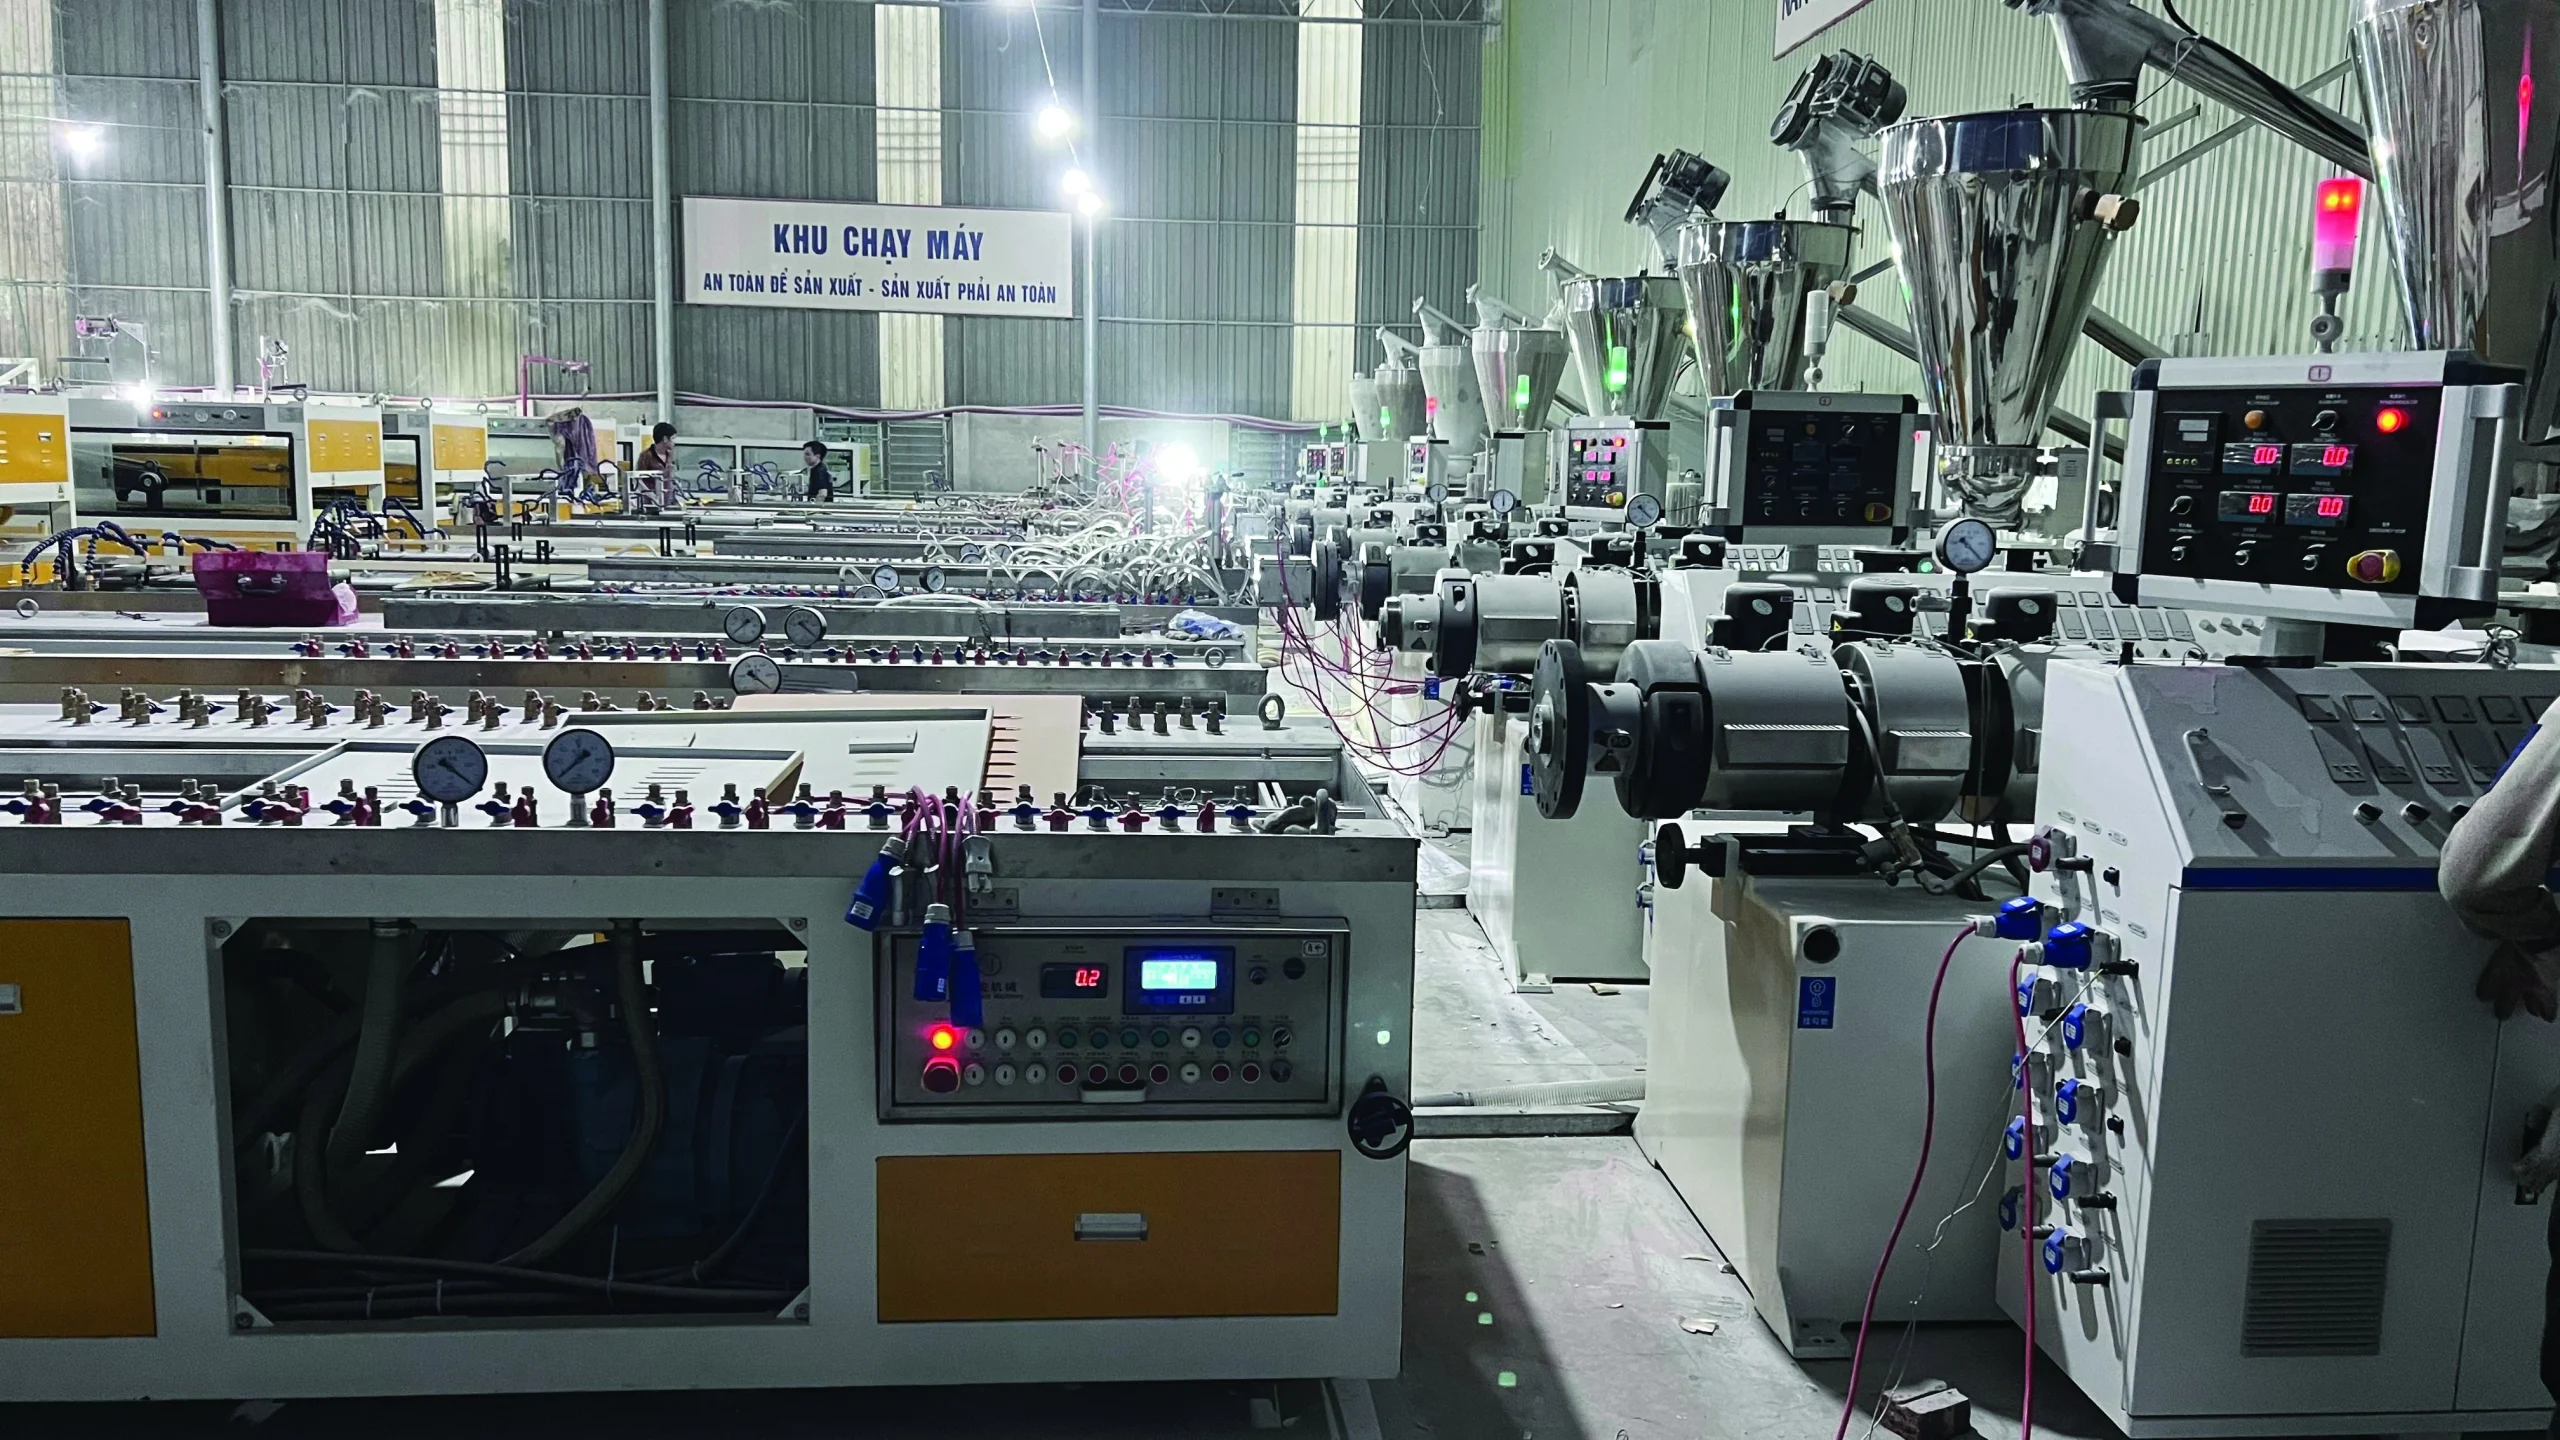
Row of extrusion line control panels at the Pharaon plant
Lamination

15 offline lines

Laminate accessory profiles and fluted boards in the same films used on flat panels.
Pharaon PVC and WPC wall panel factory production line in Vietnam
Throughput

1,700 m² per machine per day

Sustained output per line, which is what makes phased delivery predictable.
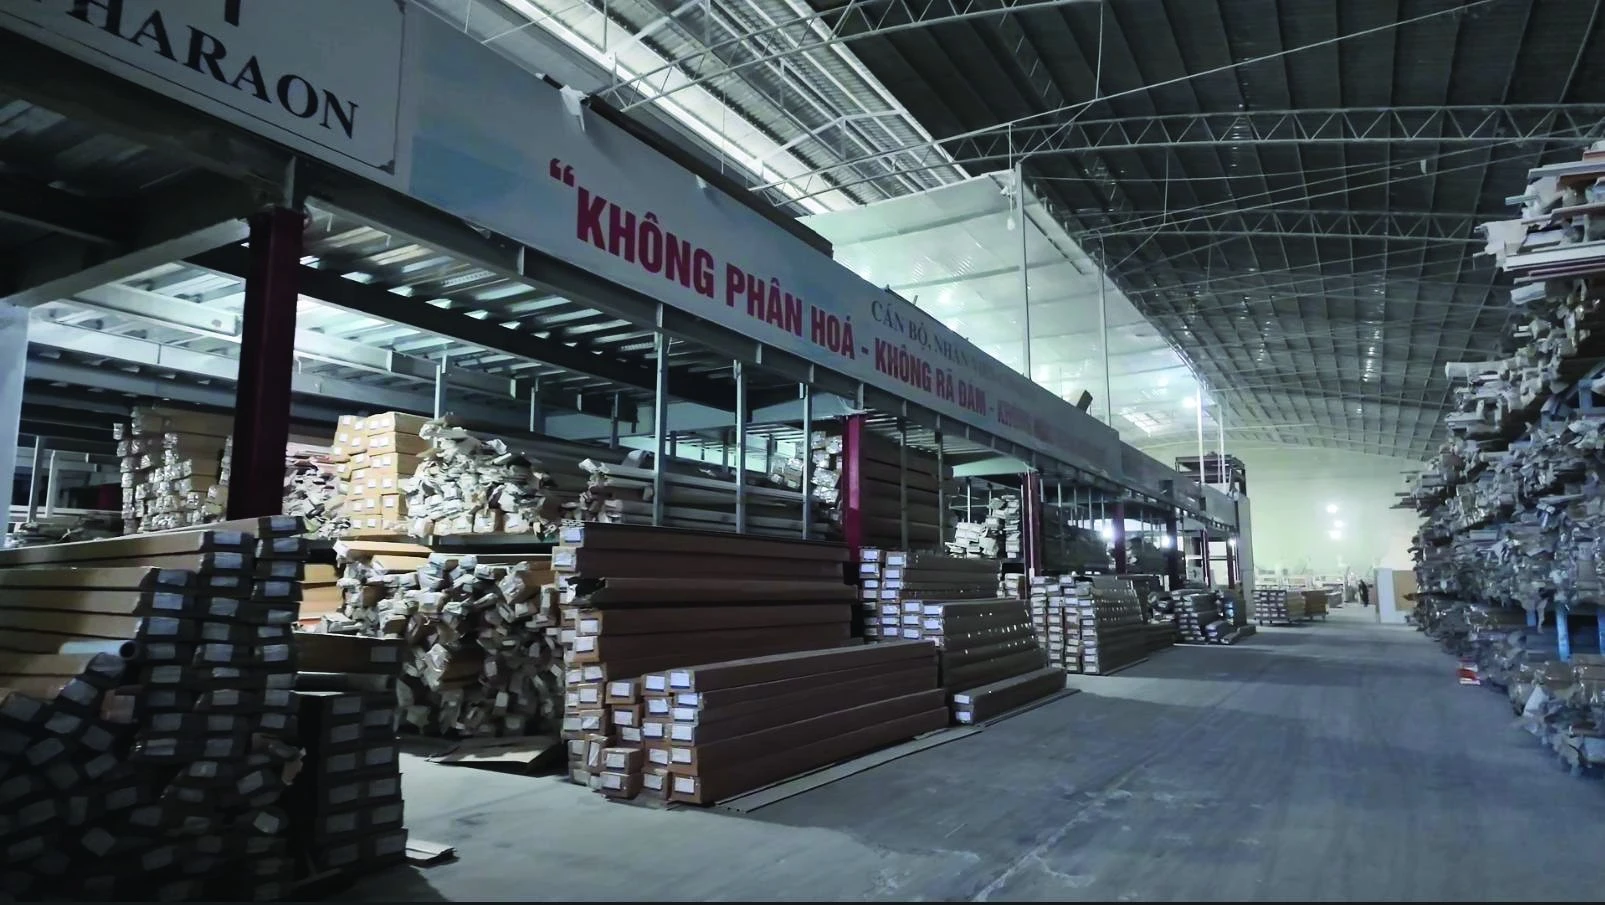
Finished Pharaon panels and profiles stacked in the plant warehouse
Layout

4 workshops on one site

16,000 m² at Phú Xuyên, Hanoi, with finished goods held on the same site.
Plant 1

Phú Xuyên, Hanoi

Site area16,000 m²
Production workshops4
Nano extrusion lines25
Stone-grain PVC extrusion1
Offline lamination lines15
Output per line1,700 m² per machine per day
Rated annual output62,000 tonnes

The 15 offline lines matter more than they sound: they laminate accessory profiles in the same films as the flat panels, which is how a cornice ends up matching the wall beneath it.

Row of extrusion line control panels at the Pharaon plant
Plant 2

Ninh Bình — in development

A second plant is being built at Lot CN04.2.2, Dong Van III Supporting Industrial Park, Tien Noi, Duy Tien, Ninh Binh, on an 85,000 m² site: 50 machines and a rated 124,000 tonnes a year. We describe this as planned capacity, not current capacity.

YearExtrusion machinesRated output / yearWorkshop area
2022612,000 t5,000 m²
20231326,000 t8,000 m²
20241734,000 t12,000 m²
20252562,000 t16,000 m²
2026 (planned)50124,000 t85,000 m² – plant 2
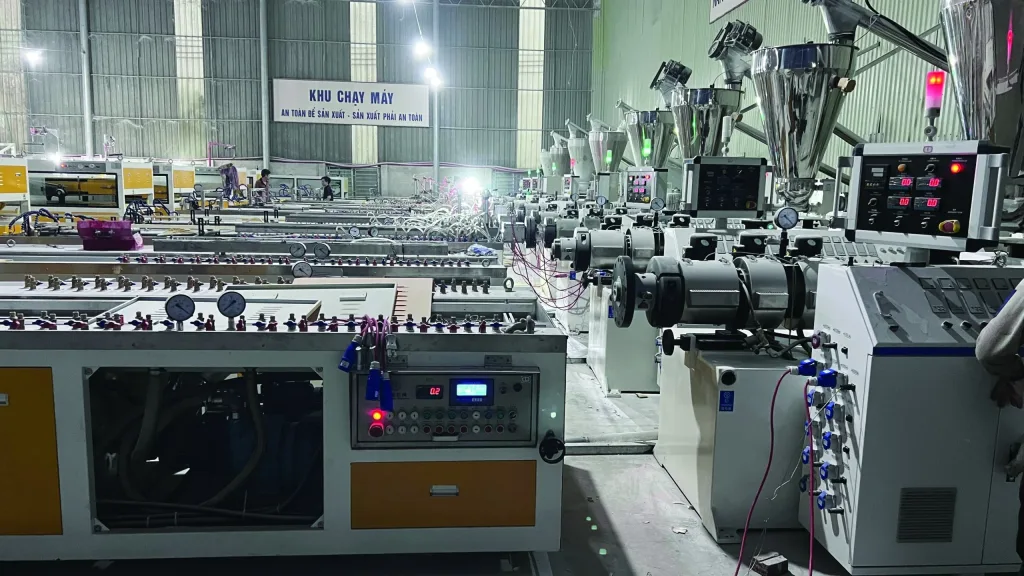
Pharaon PVC and WPC wall panel factory production line in Vietnam
Inputs and handling

Materials, storage, safety

  • Substrate resin and surface films bought to specification and checked on arrival
  • Film batches controlled tightly — a mid-order film change is what produces a shipment that does not match the sample
  • Finished goods picked by SKU and finish code, in fixed pack quantities
  • Operators issued PPE, trained on a recurring schedule and supervised on the extrusion floor
  • Set up to host buyer supplier audits

The extrusion process is run for energy efficiency and offcut recovery. We do not currently publish third-party environmental certification — ask us for the status rather than assuming it exists.

Next

How we control quality